
Guide Navigation – Table of Contents
- 1. Minimum Order Quantities & Fast Lead Times
- 2. Why Choose Tablet Manufacturing for Your Supplement Brand
- 3. Comprehensive Tablet Manufacturing Process
- 4. Specialized Tablet Types
- 5. Tablet Customization Options: Shapes, Sizes, Coatings & Colors
- 6. Custom Branding, Printing & Labeling Services
- 7. Quality Systems & International Certifications
- 8. Packaging Solutions & Bottling Integration
- 9. Our Onboarding Process: From R&D to Delivery
1. Tablet Supplement Manufacturing: Minimum Order Quantities & Fast-Track Lead Times
In the competitive nutraceutical market, speed, flexibility, and predictable costs are essential for success. Terrawell provides transparent and efficient tablet manufacturing services to help your brand scale confidently with minimal inventory risk.
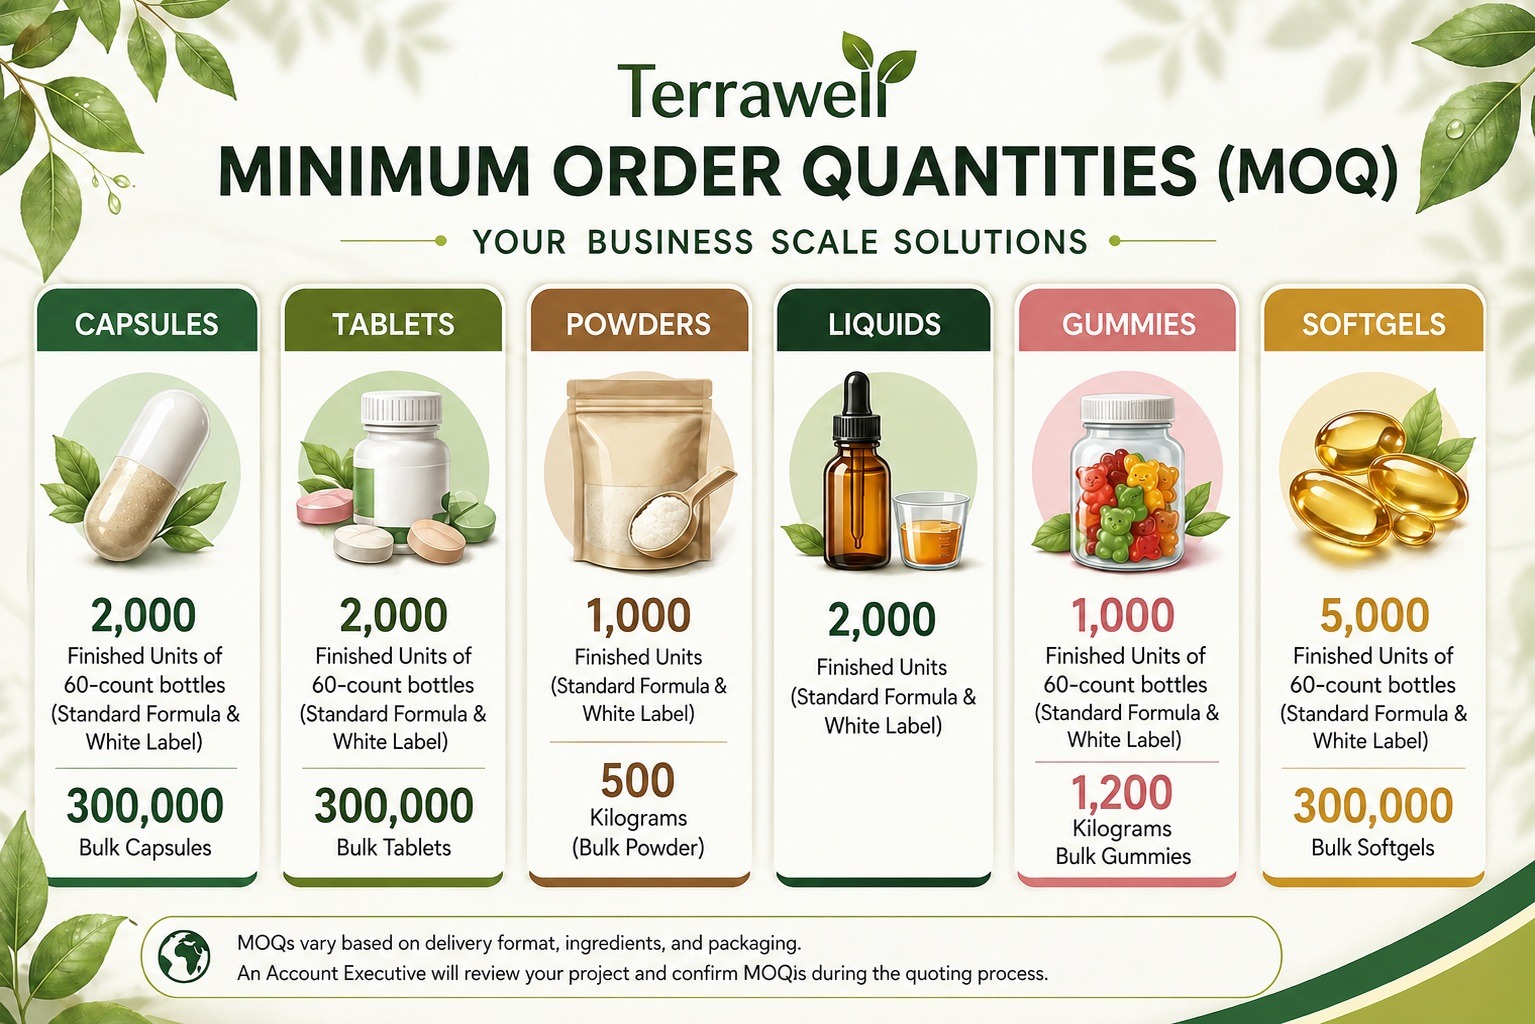
Transparent MOQs and Production Timelines
| Performance Indicator | Our Standard Commitment |
|---|---|
| Minimum Order Quantity (Bulk Tablets) | 300,000 tablets |
| Minimum Order Quantity (Finished Bottles) | 2000 bottles (60 tablets per bottle) — available for existing formulas |
| First-Time Order Lead Time | 4 – 5 weeks (from concept approval to delivery) |
| Repeat Order Lead Time | 3 – 4 weeks (with accurate forecasting) |
Expert Tip: Seasonal demand peaks (cold & flu season, back-to-school, and holidays) can affect raw material availability. We recommend placing orders 8–10 weeks in advance during high-demand periods to ensure on-time delivery.
For qualified new clients or strategic partnerships, we can discuss flexible MOQ options on select formulations. Contact us to review your project requirements.
2. Why Choose Tablet Manufacturing for Your Supplement Brand
Tablets remain one of the most popular and cost-effective delivery forms in the nutraceutical industry. At Terrawell, we help brands leverage the unique advantages of tablet manufacturing to achieve better margins, stronger consumer appeal, and greater market flexibility.
Key Advantages of Tablet Supplements
Superior Cost Efficiency
Tablet production costs are typically 30–50% lower than gummies or softgels, while offering excellent scalability for both small and large runs.
Longer Shelf Life
Tablets often achieve 24–36 months of stability with proper formulation and packaging, reducing inventory risk and waste.
Precise Dosing & Consistency
Advanced compression technology ensures every tablet delivers exactly the intended dosage with minimal variation.
Consumer Convenience & Trust
Familiar format, easy to swallow, portable, and no refrigeration required — tablets build immediate consumer confidence.
Tablet vs Other Delivery Forms
| Delivery Form | Shelf Life | Cost Efficiency | Dosage Accuracy | Consumer Preference |
|---|---|---|---|---|
| Tablets | Excellent (24–36 months) | High | Very High | High |
| Capsules | Good | Medium | High | High |
| Gummies | Moderate | Low | Variable | Very High |
| Softgels | Good | Low | High | Medium-High |
Whether you are launching a new brand or expanding an existing line, tablets offer an excellent balance of cost efficiency, stability, and consumer trust — making them one of the smartest choices for scalable supplement manufacturing.
3. Comprehensive Tablet Manufacturing Process
Tablet production is a sophisticated multi-step process that transforms raw powders into consistent, high-quality finished tablets. At Terrawell, we utilize advanced equipment and strict process controls to ensure every batch meets exact specifications for weight, hardness, dissolution, and stability.
Key Stages of Tablet Manufacturing
1. Granulation
Raw ingredients are transformed into uniform granules to improve flowability and compressibility. We use both wet granulation (for better binding) and dry granulation (for heat/moisture-sensitive formulas).
2. Drying & Milling
Precise moisture control and particle size reduction ensure consistent granule quality. Our milling systems achieve optimal particle distribution for excellent tablet uniformity.
3. Blending
High-efficiency blenders create homogeneous mixtures, guaranteeing that every tablet contains the exact ratio of active ingredients and excipients.
4. Compression
State-of-the-art rotary tablet presses compress granules into tablets with precise weight, hardness, and thickness control. Real-time monitoring ensures consistent quality across the entire batch.
5. Coating (Optional)
Film, enteric, or extended-release coatings are applied to enhance appearance, mask taste, protect ingredients, or control release profiles.
Why Process Control Matters
Every stage is monitored with strict in-process controls including moisture testing, blend uniformity, weight variation, hardness, and friability checks. This comprehensive approach minimizes defects and ensures your tablets consistently meet label claims and regulatory standards.
Expert Tip: Proper granulation and compression parameters are critical for high-dose or multi-ingredient formulas. Poor process control can lead to capping, sticking, or inconsistent dissolution — issues we actively prevent through rigorous optimization.
From simple immediate-release tablets to complex coated or multi-layer formulations, our experienced team delivers reliable, scalable tablet manufacturing with pharmaceutical-grade quality.
4. Specialized Tablet Types
Beyond standard immediate-release tablets, Terrawell offers a range of specialized tablet formats to meet different consumer needs, formulation requirements, and market positioning goals.
Common Specialized Tablet Formats
Chewable Tablets
Pleasant-tasting tablets designed for easy chewing. Ideal for children, seniors, and those who have difficulty swallowing pills. We optimize texture and flavor masking for excellent consumer compliance.
Effervescent Tablets
Dissolve quickly in water to create a fizzy, refreshing beverage. Offers fast absorption and improved taste for vitamins, minerals, and digestive support formulas.
Oral Disintegrating Tablets (ODT)
Dissolve rapidly on the tongue within 30–60 seconds without water. Perfect for on-the-go use and consumers who dislike swallowing tablets.
Enteric-Coated Tablets
Coated to resist stomach acid, protecting sensitive ingredients like probiotics and enzymes until they reach the intestines for optimal absorption.
Extended / Time-Release Tablets
Designed to release active ingredients gradually over several hours. Reduces dosing frequency and improves patient compliance for daily supplements.
Each specialized format requires specific formulation expertise, excipient selection, and process optimization. Our team works closely with you to select the most suitable type based on your target market, active ingredients, and desired release profile.
Expert Recommendation: For acid-sensitive ingredients such as probiotics or digestive enzymes, enteric coating is often the best choice. For convenience-focused products, effervescent or ODT formats can significantly improve consumer satisfaction and repeat purchase rates.
Whether you need simple chewables for kids or advanced time-release formulas for premium positioning, Terrawell delivers consistent, high-quality specialized tablets that help your brand stand out.
5. Tablet Customization Options: Shapes, Sizes, Coatings & Colors
One of the greatest advantages of tablet manufacturing is the high degree of customization possible in appearance, functionality, and consumer experience. At Terrawell, we help brands create distinctive tablets that not only deliver precise dosing but also strengthen visual identity, improve swallowability, and meet clean-label demands.
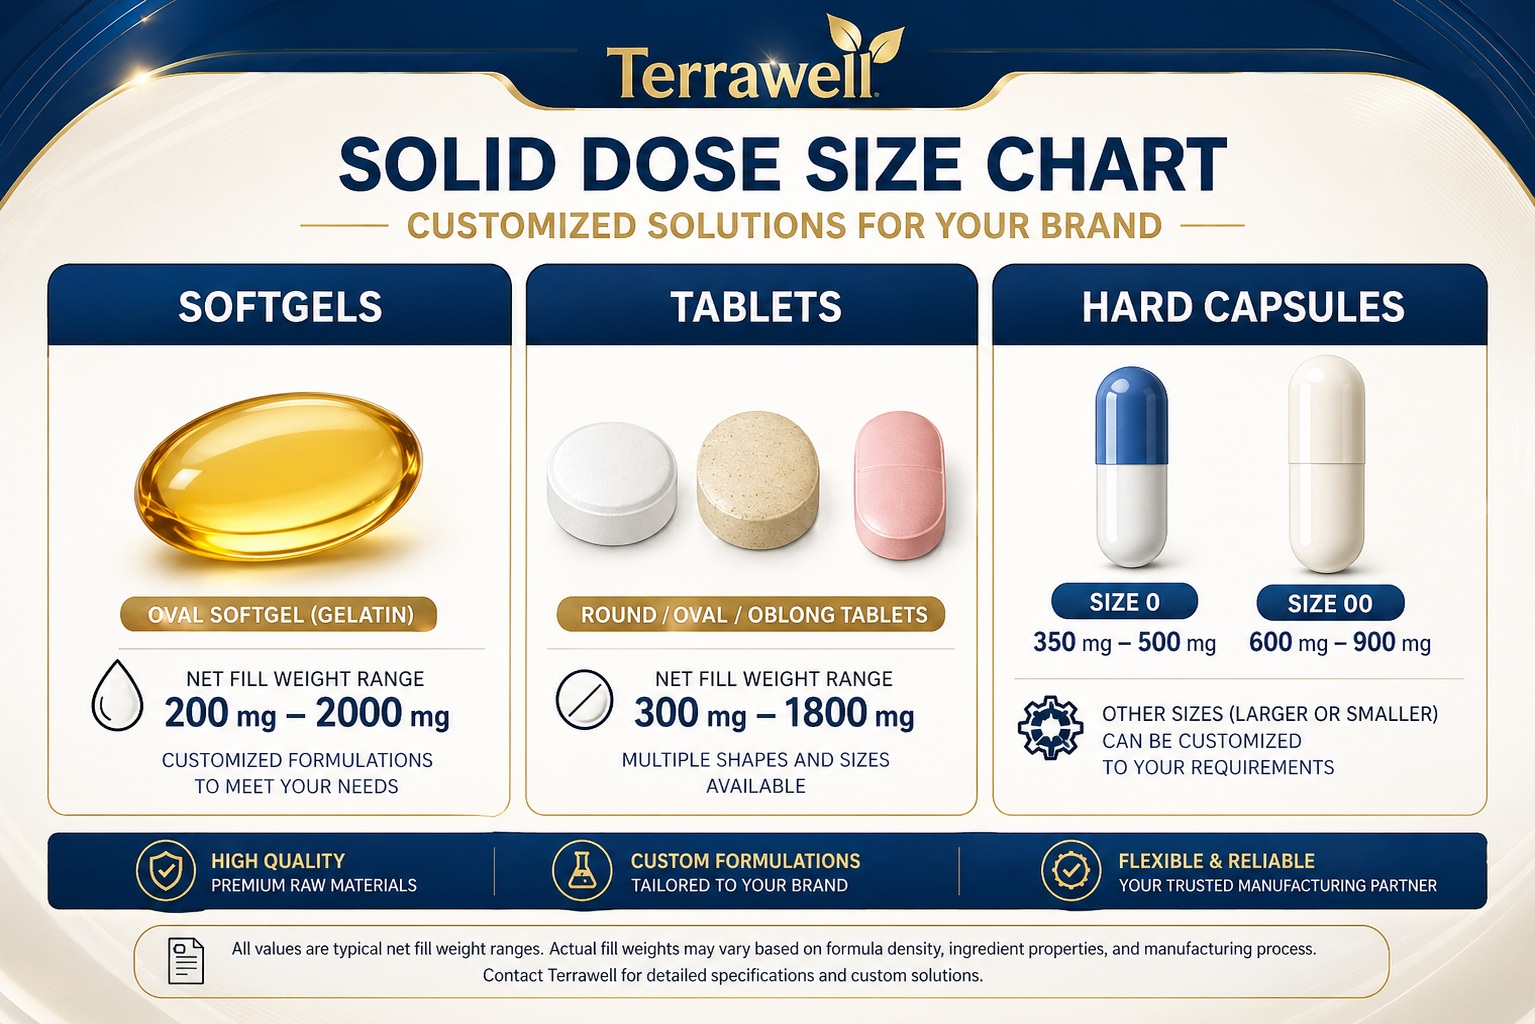
Tablet Size & Weight Options
Proper tablet size selection is critical for dosing accuracy, swallowability, manufacturing efficiency, and consumer acceptance. We optimize size based on total active ingredient weight, excipient requirements, and target user group (children, adults, or seniors).
| Typical Weight Range | Diameter (mm) | Thickness (mm) | Best For |
|---|---|---|---|
| 200 – 500 mg | 8 – 10 mm | 3 – 5 mm | Children’s formulas, low-dose supplements, easy swallowing |
| 500 – 800 mg | 10 – 12 mm | 4 – 6 mm | Standard adult multivitamins and daily supplements |
| 800 – 1200 mg | 12 – 14 mm | 5 – 7 mm | High-potency formulas and combination products |
| 1200 – 1800 mg | 14 – 16 mm | 6 – 8 mm | High-dose specialty supplements (often recommended in oval or caplet shape) |
| 1800 mg+ | 16 mm+ | 8 mm+ | Extra large or complex formulations – requires custom tooling and engineering review |
*Final tablet dimensions are optimized during the R&D phase based on powder compressibility, target dose, and desired swallowability. For weights above 1800 mg, we recommend oval or caplet shapes and will conduct additional compression studies.
Expert Tip: Larger tablets (1200 mg+) are often more comfortable to swallow when designed as oval or caplet rather than round. We always balance size with consumer experience during size selection.
Shape & Size Customization
Tablet shape and size directly impact swallowability, brand recognition, and production efficiency. We work with you to select the optimal geometry for your target audience.
Round Tablets
Most cost-effective and widely used. Excellent mechanical stability during compression and coating. Ideal for standard supplements.
Oval / Caplet Tablets
Easier to swallow than round tablets of similar weight. Preferred for larger doses or consumers who have difficulty swallowing pills.
Oblong & Scored Tablets
Unique appearance for strong brand differentiation. Scored lines allow flexible dosing (half or quarter tablets).
Expert Tip: Oval and caplet shapes often provide better swallowability for larger-dose formulas. For children or seniors, smaller sizes with smooth edges are recommended.
Coating Technologies
Coating enhances tablet performance, appearance, and functionality. We offer multiple options tailored to your formulation.
- Film Coating: Thin polymer layer that improves swallowability, masks taste, and protects against moisture and light while maintaining fast release.
- Enteric Coating: Protects acid-sensitive ingredients (probiotics, enzymes) from stomach acid for targeted intestinal release.
- Extended / Time-Release Coating: Controls release over hours, improving compliance by reducing dosing frequency.
Coloring Options & Clean Label Solutions
Color plays a key role in brand recognition and shelf appeal. With growing consumer demand for clean-label products, we support both vibrant synthetic options and natural pigments that align with “No Artificial Colors” claims under current FDA guidance.
| Color Source | Typical Colors Produced | Type | Key Advantages | Notes / Considerations |
|---|---|---|---|---|
| Beetroot Red | Red to Pink | Natural (Plant) | Vibrant, clean-label friendly | Excellent for “No Artificial Colors” claims; stable in many formulas |
| Spirulina Extract | Blue to Green | Natural (Algae) | Unique blue shades, nutrient-rich | Recently expanded FDA use; supports clean label positioning |
| Turmeric / Curcumin | Yellow to Orange | Natural (Plant) | Antioxidant properties | Popular for health-focused brands; may have slight flavor impact |
| Annatto | Orange to Yellow | Natural (Seed) | Stable, warm tones | Good alternative to synthetic yellows |
| Beta-Carotene | Orange to Yellow | Natural (Plant/Carotenoid) | Vitamin A precursor | Nutritionally beneficial; widely accepted |
| FD&C Colors (e.g. Red 40, Yellow 5) | Various bright shades | Synthetic (Petroleum-based) | Intense, consistent, cost-effective | Rare allergic reactions possible; being phased down in many markets |
Expert Recommendation: For premium and clean-label brands, we recommend combining natural pigments (such as beetroot red or spirulina) with film or enteric coating. This approach delivers attractive, functional tablets while supporting “No Artificial Colors” labeling claims and meeting current FDA flexibility on petroleum-based dyes.
From simple round film-coated tablets to complex multi-layer scored enteric tablets with natural colors, our customization capabilities help your product stand out while maintaining excellent manufacturability and consumer appeal.
6. Custom Branding, Printing & Labeling Services
In today’s competitive supplement market, strong visual identity and professional presentation are essential for standing out on the shelf and building consumer trust. Terrawell provides comprehensive customization services to help your tablet products reflect your brand personality while meeting all regulatory requirements.
Tablet Printing & Imprinting
We offer high-precision tablet imprinting using edible inks to apply your logo, brand name, dosage strength, or other identifiers directly onto the tablet surface. This serves as both a powerful branding tool and an effective anti-counterfeiting measure.
Professional Label Design & Printing
Design Elements
- FDA-compliant Supplement Facts panel
- Eye-catching graphics and brand-consistent typography
- High-resolution product images and icons
- Clear ingredient lists and usage instructions
Compliance & Regulatory Support
- Structure/function claim review
- Allergen declarations and warnings
- Batch coding, lot tracking, and expiration dating
- Full FDA and international compliance check
Material & Finish Options
- Paper labels for standard applications
- Synthetic waterproof materials for durability
- Clear labels for product visibility
- Premium finishes: glossy, matte, metallic foil, embossing
Our in-house design and regulatory team ensures every label is both visually compelling and fully compliant, reducing risk and accelerating your time to market.
From elegant film-coated tablets with custom imprinting to premium packaging with eye-catching labels, we help transform your tablets into distinctive, shelf-ready products that reinforce your brand identity and build consumer confidence.
7. Quality Systems & International Certifications
At Terrawell, quality is the foundation of every tablet we produce. Our facilities operate under strict pharmaceutical-grade standards with multiple international certifications to ensure purity, potency, safety, and batch-to-batch consistency.
Key Certifications & Quality Systems
- GMP (Good Manufacturing Practice) — Full adherence to current GMP standards with documented SOPs and complete batch traceability from raw materials to finished tablets.
- BRCGS Certification — Global food safety standard that exceeds minimum regulatory requirements, providing extra confidence for retailers and consumers.
- Organic, Kosher, and Halal Certifications — Available to help you access specialized market segments and meet diverse dietary preferences.
Three-Tier Quality Control Process
Incoming Inspection
Every raw material and excipient is rigorously tested for identity, purity, potency, and microbial contamination before entering production.
In-Process Monitoring
Real-time checks during granulation, blending, compression, and coating ensure weight uniformity, hardness, thickness, and dissolution performance.
Final Batch Release
Comprehensive laboratory analysis including assay, dissolution, friability, and microbial testing. A full Certificate of Analysis (CoA) is issued for every shipment.
Additional Value: We provide accelerated stability testing to simulate different environmental conditions and predict 24–36 month shelf life performance. This is particularly important for coated and high-potency tablet formulations.
Full digital traceability allows us to track every ingredient — from specific excipient lots to the final compressed tablet — within minutes.
8. Packaging Solutions & Bottling Integration
Proper packaging protects tablet stability, enhances brand perception, and optimizes shipping costs. Terrawell offers flexible, high-quality packaging solutions tailored to your product requirements and target market.
Primary Packaging Options
- HDPE / PET Bottles — Available in amber, white, or clear with child-resistant or induction-sealed caps. Excellent protection against moisture and light while maintaining cost efficiency.
- Blister Packs (Alu-Alu or PVC/PVDC) — Superior moisture barrier and individual dosing convenience. Ideal for travel, promotional samples, or compliance-focused products.
- Bulk Supply — Finished tablets packed in double-lined pharmaceutical-grade bags inside heavy-duty cartons, ready for your own downstream bottling or packaging lines.
Optimized Bottling Configurations
To prevent excessive headspace (which can accelerate oxidation) or tablet damage during transport, we carefully calculate bottle size and fill count for each formulation. For example, a 60-count bottle of standard 800–1000 mg tablets typically uses a 150cc to 200cc container.
Our team optimizes these ratios to reduce shipping volume, lower costs, minimize environmental impact, and maintain product integrity throughout the supply chain.
Whether you need retail-ready bottled products, protective blister packaging, or bulk supply for your own lines, we deliver packaging solutions that balance protection, aesthetics, and efficiency.
9. Our Onboarding Process: From R&D to Delivery
Starting a new tablet manufacturing project can feel overwhelming. Terrawell simplifies the entire journey with a structured, transparent, and efficient onboarding process designed to bring your product from concept to market quickly and smoothly.
The Five-Step Partnership Journey
- Consultation & Quoting — Share your formula, concept, or even just an idea. We provide a detailed feasibility analysis and competitive quote within 48 hours.
- R&D & Sampling — Our experienced formulators develop prototypes, optimize granulation and compression parameters, test stability and dissolution, and refine until you are fully satisfied.
- Compliance & Labeling Review — We review your label design and claims for full regulatory compliance (FDA, structure/function claims, allergens, etc.) and prepare all necessary documentation.
- Mass Production — Precision tablet compression with real-time monitoring of weight, hardness, thickness, and friability. MOQ starts at 300,000 tablets (bulk) or 2000 finished bottles (for existing formulas).
- Quality Release & Shipping — Final laboratory approval, issuance of Certificate of Analysis (CoA), and global logistics support — including direct shipping to Amazon FBA or your distribution centers.
Additional Support Services
Terrawell is more than a manufacturer — we are your long-term growth partner. We offer temperature-controlled warehousing, order fulfillment, and global shipping solutions to help you scale efficiently.
Ready to Bring Your Tablet Supplement Idea to Life?
Whether you have a detailed formula or just a concept, our team is here to help you scale with confidence.
Get a detailed quote and feasibility analysis within 48 hours.
Simply send us your ingredient list (with mg per tablet), desired tablet type/size, packaging requirements, or even just your idea.
Contact Terrawell today — Let’s build your success together.